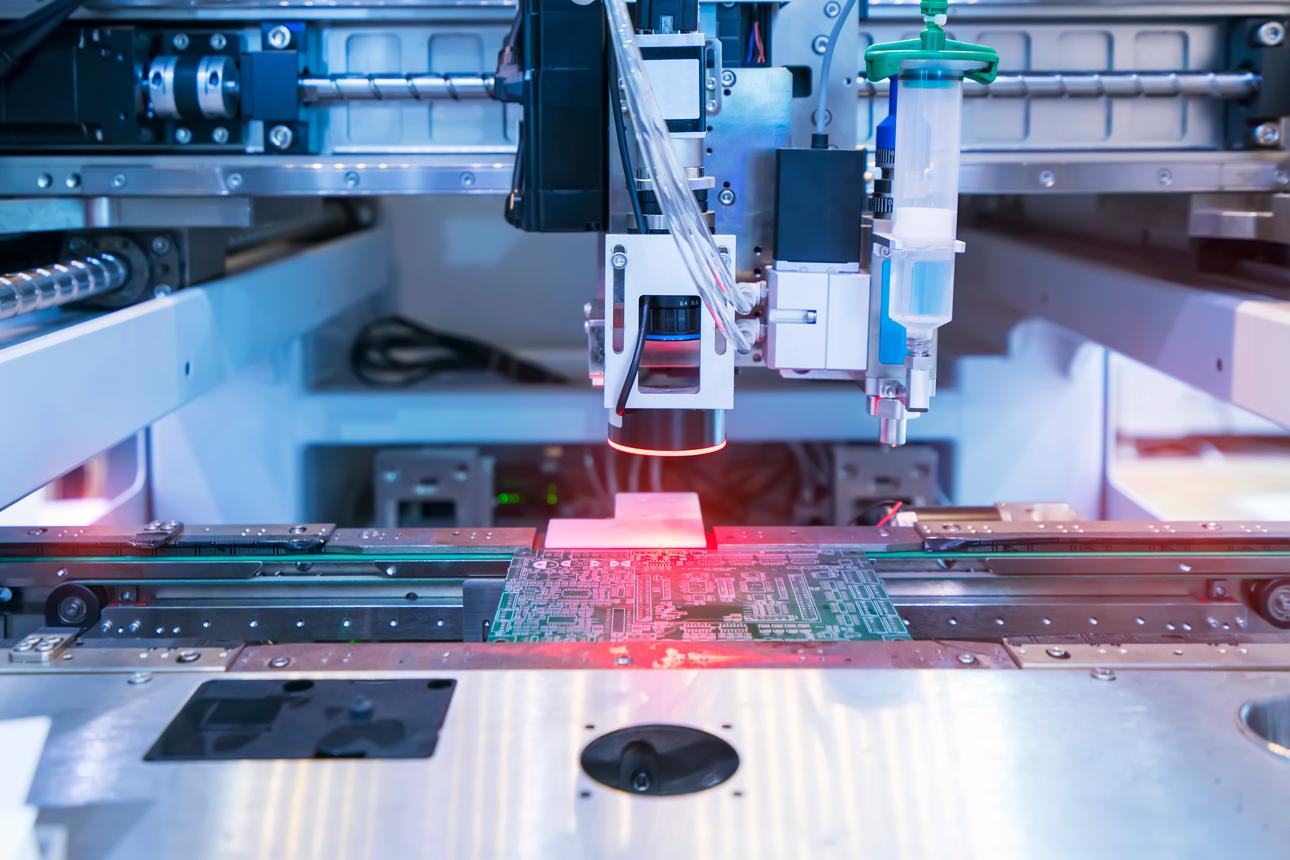
With the rapid development of industrial automation and smart manufacturing, machine vision systems are becoming increasingly important in modern production environments. They are widely used for product inspection, defect detection, barcode recognition, dimensional measurement, and automated quality control.
As the core computing platform of a machine vision system, an industrial motherboard plays an important role in ensuring stable operation and efficient image processing.
Key Requirements for Machine Vision Motherboards
1. High-Performance Processing
Machine vision applications often require real-time image analysis and data processing. Industrial motherboards equipped with Intel or AMD processors can provide the computing performance needed for image recognition, inspection, and automation tasks.
2. Multiple Expansion Interfaces
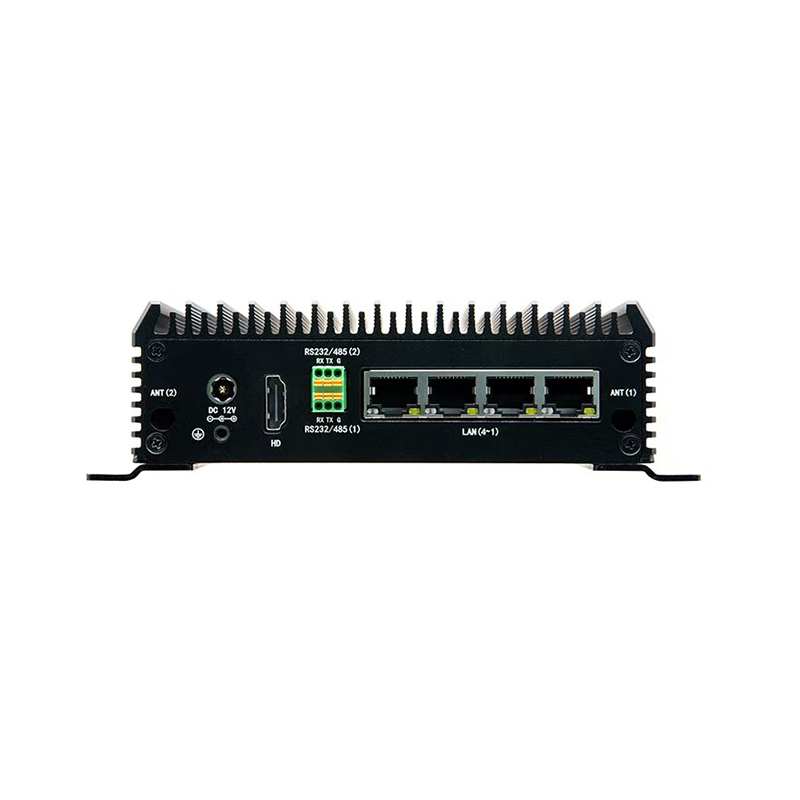
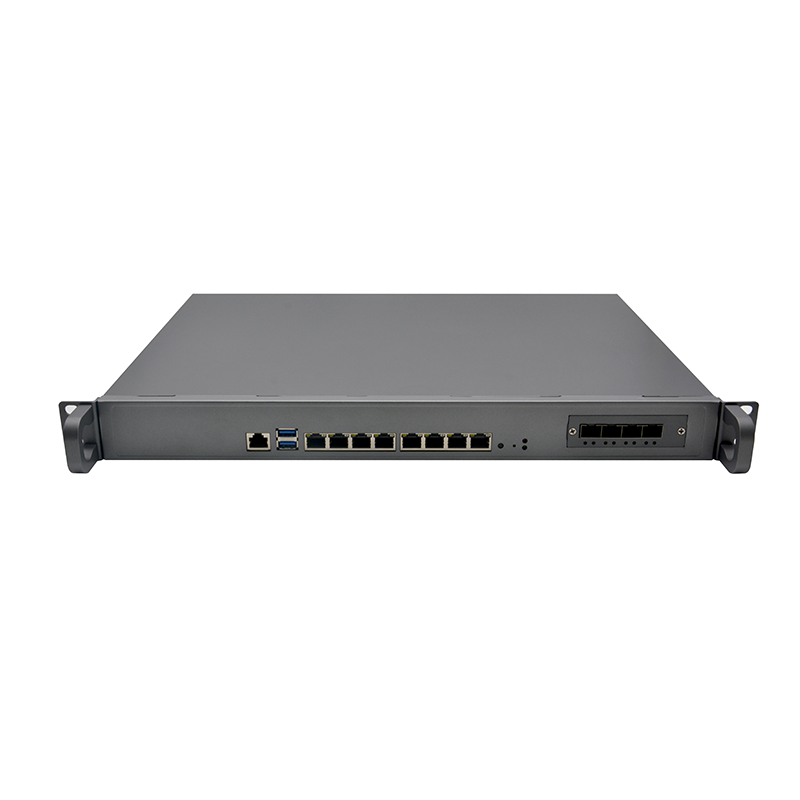
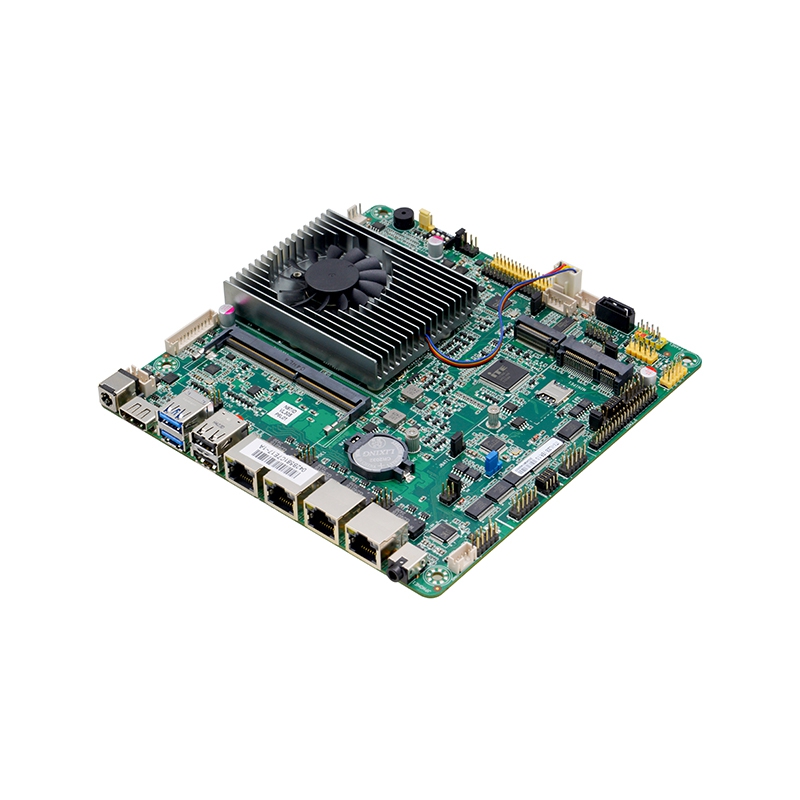
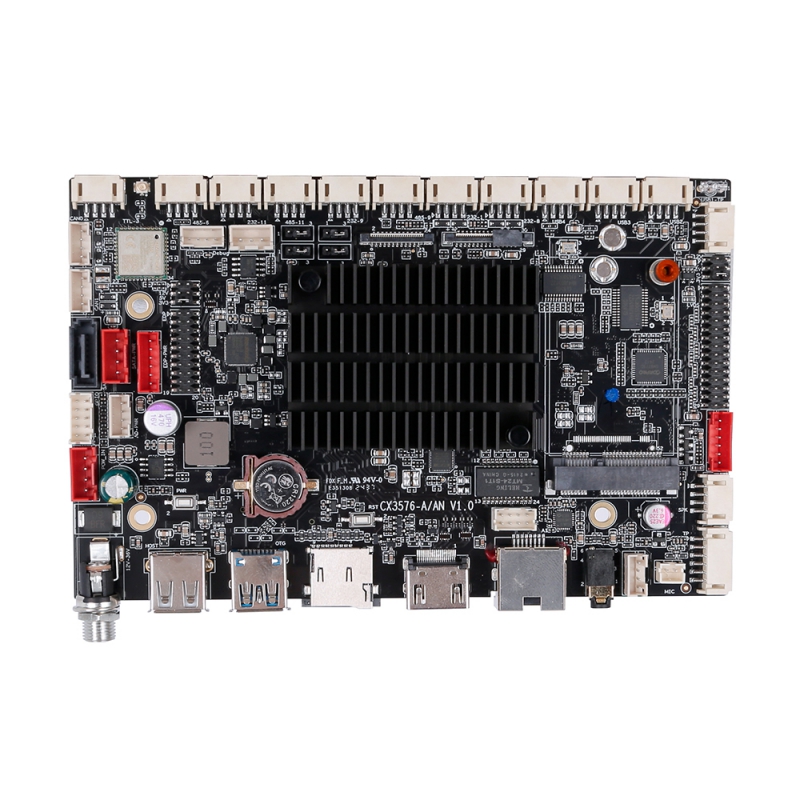
Machine vision systems may connect to industrial cameras, sensors, displays, and other peripheral devices. Multiple USB, COM, LAN, PCIe, and M.2 interfaces help support different hardware configurations and system integration requirements.
3. Stable and Reliable Operation
In industrial environments, equipment may need to operate continuously for long periods. Industrial motherboards are designed for demanding applications, with attention to system stability, component reliability, and long-term operation.
4. Flexible Form Factors and Customization
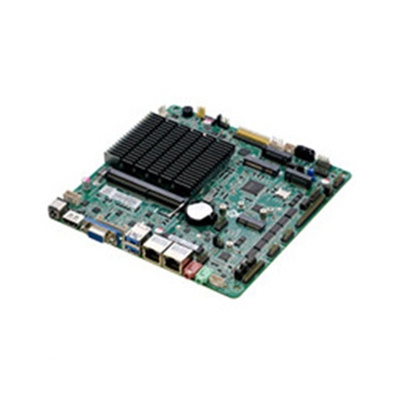
Different machine vision equipment requires different motherboard sizes and layouts. Options such as 3.5-inch, Mini ITX, Micro ATX, and ATX motherboards provide flexibility for various embedded systems and industrial computers. OEM and ODM customization can also help meet specific project requirements.
Applications in Industrial Machine Vision
Industrial motherboards can be integrated into a wide range of machine vision applications, including:
- Automated optical inspection (AOI)
- Industrial camera and image acquisition systems
- Defect detection and quality inspection
- Barcode and QR code recognition
- Intelligent manufacturing and robotic vision
- Automated production line monitoring
Choosing the Right Industrial Motherboard
When selecting an industrial motherboard for a machine vision system, manufacturers should consider CPU performance, memory capacity, expansion interfaces, display outputs, operating temperature, and long-term product availability.
The right motherboard can help improve system integration, support reliable image processing, and provide a flexible foundation for future equipment upgrades.
Senbainno provides industrial motherboard solutions in various form factors, supporting embedded computing, industrial automation, and machine vision applications. We also offer OEM/ODM customization to meet different project requirements.
Contact Senbainno to discuss your industrial motherboard requirements for machine vision systems.
Mobile/Whats App: +86 159 1948 2214
Website: www.senbatech.com


 WhatsApp

 Teamas

